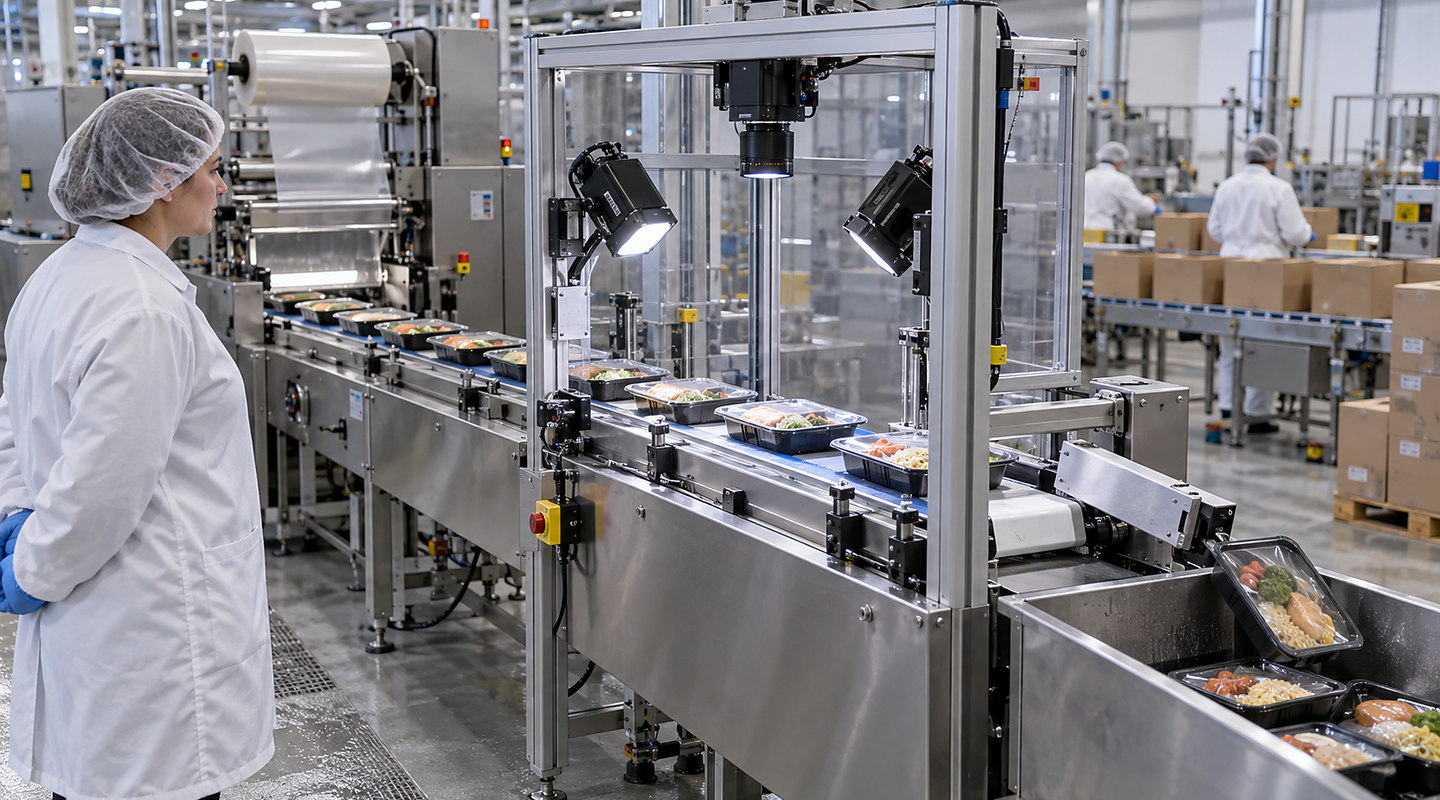
Pouch Checkweighers: How the Process Works
Follow the operating sequence for pouch checkweighers, from preparing the input and controlling the main task to handling exceptions and checking results.
Pouch Checkweighers should be considered as part of a complete production sequence: inputs are prepared, the main task is controlled, exceptions are handled and results are checked.
For your application, the important details include filled pouches, flexible pack shape and pouch-to-pouch tare variation, smallest meaningful weight difference and acceptance window, pack dimensions, stability and conveyor presentation, and line speed, spacing, vibration and transfer conditions.
Understand the complete route from input to accepted output — Pouch Checkweighers
Plan pouch checkweighers around the smallest meaningful weight difference, normal product and tare variation, pack transfer, line speed, reject confirmation and traceable test evidence. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

Four clear stages for pouch checkweighers
At each stage, you can review how filled pouches, flexible pack shape and pouch-to-pouch tare variation and test packs, challenge method, records and production response affect the next commitment.
- 01
Measure Normal Product and Packaging Variation
Share representative packs, measured weight variation and known test packs, including the normal range for filled pouches, flexible pack shape and pouch-to-pouch tare variation and the difficult smallest meaningful weight difference and acceptance window cases.
- 02
Trial the Real Pack Range At Intended Line Conditions
Compare suitable methods and use focused trials to show how each option performs against pack dimensions, stability and conveyor presentation.
- 03
Integrate Transfers, Controls, Rejection and Confirmation
Connect the equipment to your line, services and controls while resolving line speed, spacing, vibration and transfer conditions for day-to-day operation.
- 04
Challenge Known Weight Faults and Retain Agreed Test Results
Confirm reject device, removal confirmation and reject-bin state, then complete and record test packs, challenge method, records and production response before your operating team takes over.
Decisions and results stay connected
| Stage | What happens | What you can review |
|---|---|---|
| Measure Normal Product and Packaging Variation | Confirm the requirements for dynamic weighing of filled pouches, the operating range and the definition of a good result. | Your samples, current information and any points that still need confirming. |
| Trial the Real Pack Range At Intended Line Conditions | Compare workable methods using filled pouches, flexible pack shape and pouch-to-pouch tare variation and smallest meaningful weight difference and acceptance window from your real production. | The trial method, observations and reason for the recommended route. |
| Integrate Transfers, Controls, Rejection and Confirmation | Resolve pack dimensions, stability and conveyor presentation, line speed, spacing, vibration and transfer conditions and the physical, control, safety and data connections. | The agreed layout, line connections and any changes from the proposal. |
| Challenge Known Weight Faults and Retain Agreed Test Results | Check normal, difficult and fault conditions before your team takes over the system. | Results for reject device, removal confirmation and reject-bin state and test packs, challenge method, records and production response, plus actions and operating information. |
Keep connected responsibilities clear
Your final pouch checkweighers scope must also account for reject device, removal confirmation and reject-bin state, test packs, challenge method, records and production response, current regulations and the conditions at your site.
- A checkweigher can only detect a fault that creates a meaningful weight difference.
- Normal product and packaging variation must be understood before setting an acceptance window.
- A reject signal is not proof that the failed pack was physically removed and confirmed.